Low dissolved oxygen
Coordinate transfer, can purging, filling and end placement to reduce oxygen exposure.
Beer solution / Can container
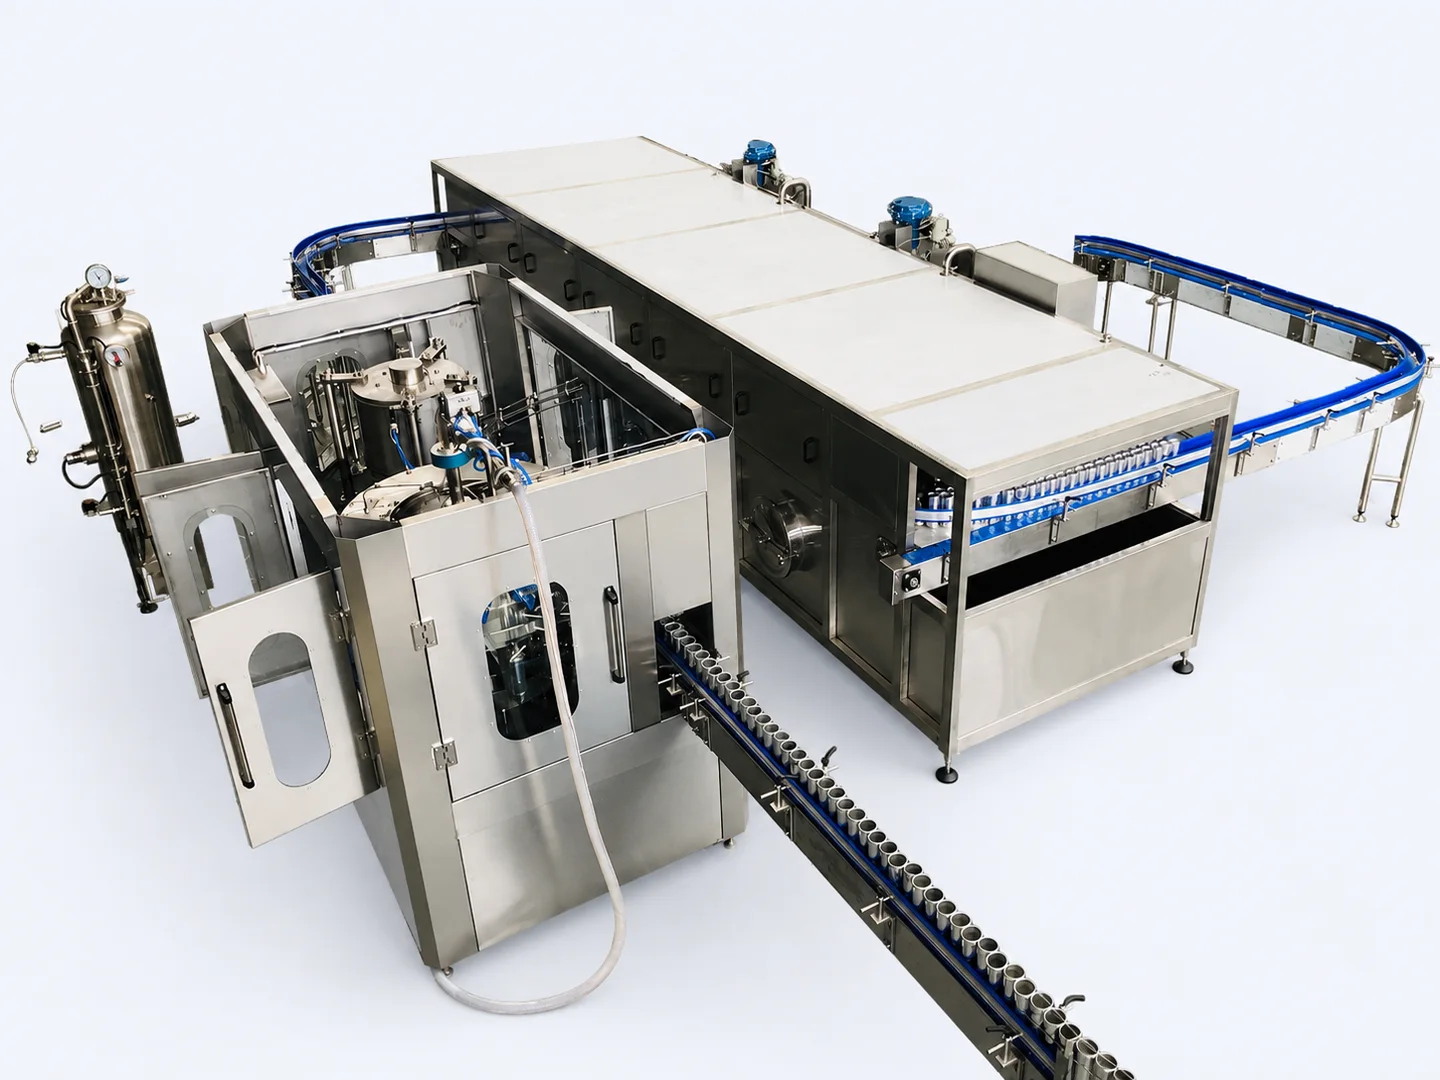
Connect empty-can depalletizing and rinsing to protected beer transfer, low-oxygen filling, can-end seaming, inspection and final packaging.
Request a line proposalComplete solution
Engineer the can and end as one package. Beer condition, filling temperature, carbonation, foam behaviour, oxygen-control target and seam standard shape the filling block and downstream route.
Engineering signals
Each decision connects beer condition and package performance to a controllable part of the line.
Coordinate transfer, can purging, filling and end placement to reduce oxygen exposure.
Depalletize, convey, invert and rinse cans without damaging the body or flange.
Balance product temperature and pressure to control foam and fill repeatability.
Match the can body, end and seamer setup, then define inspection and teardown checks.
Configure warming or tunnel pasteurization only where the product plan requires it.
Complete line scope
The approved can body and end, beer condition, seam criteria and pack format define the final line scope.
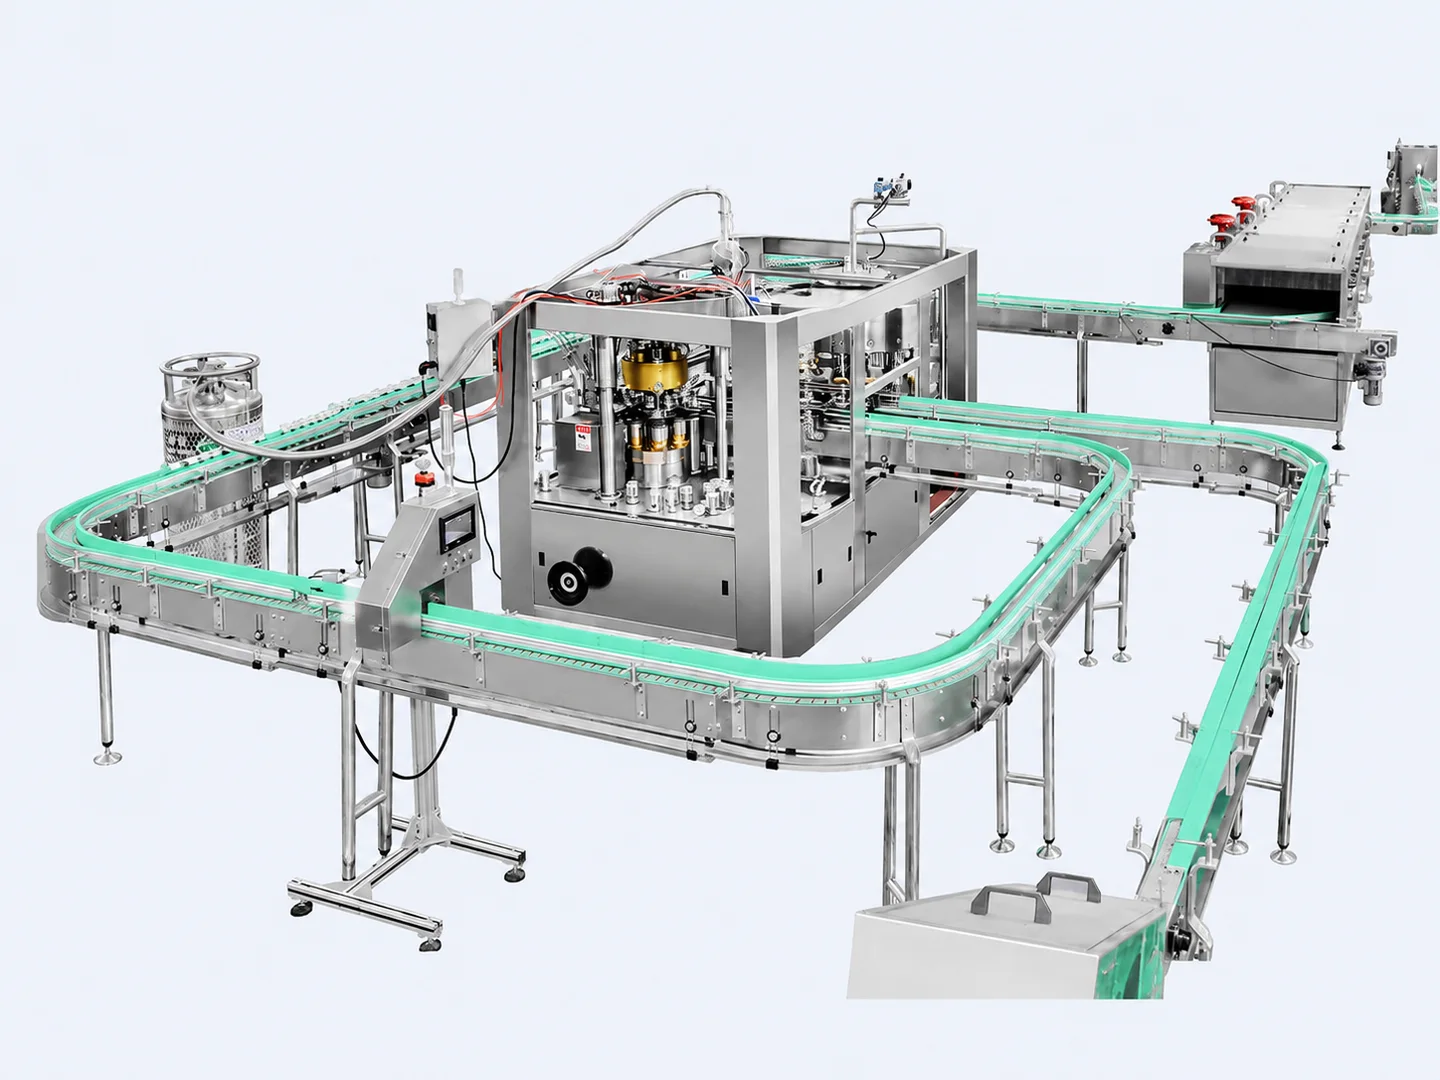
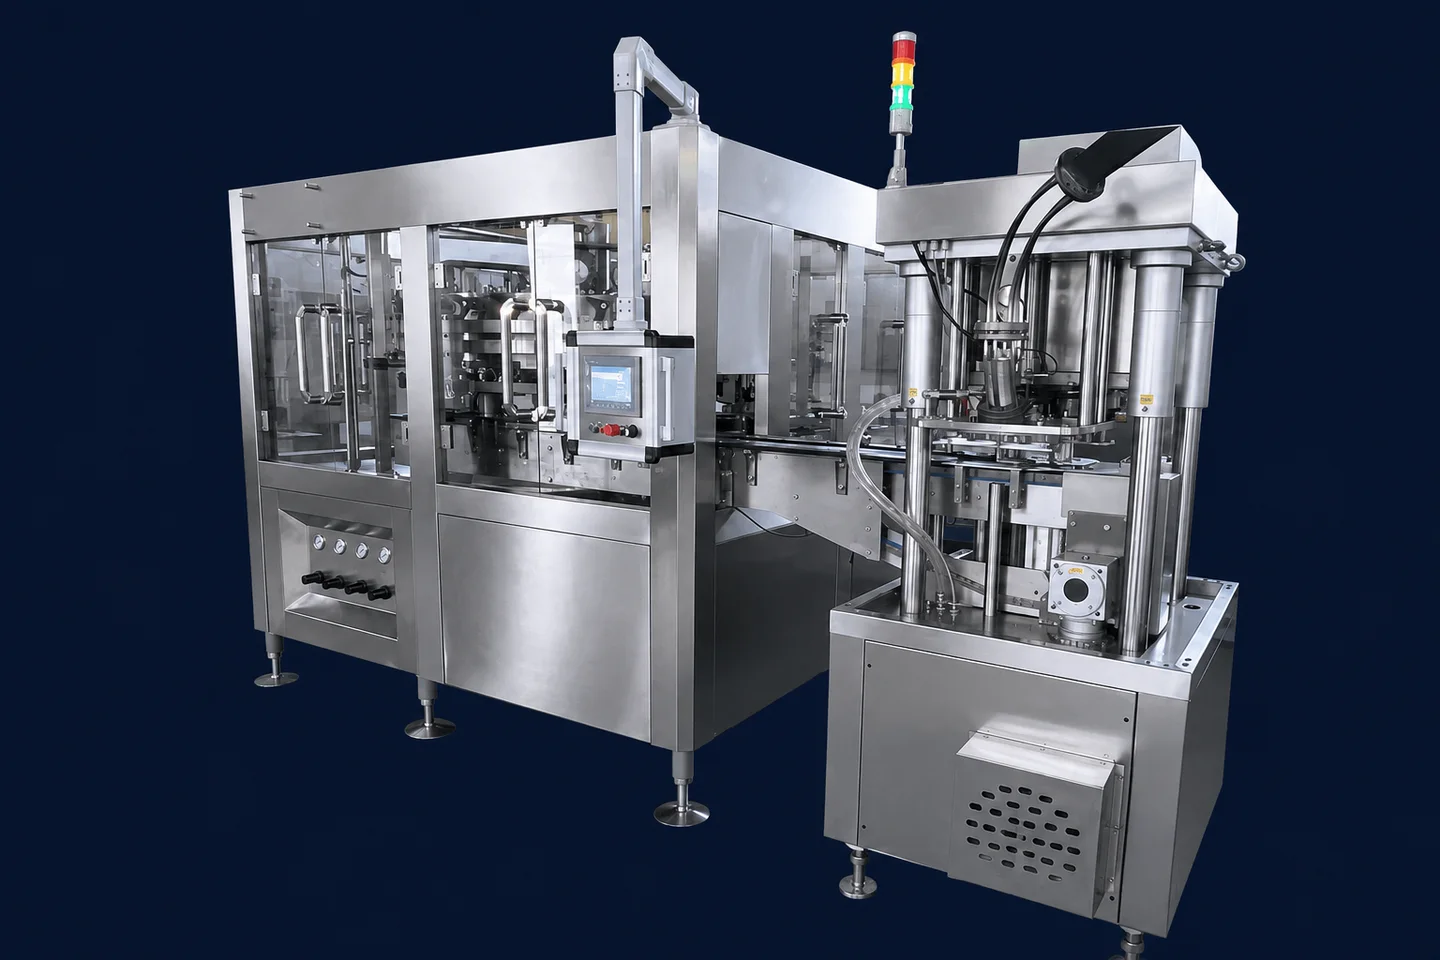
Empty-can depalletizing, accumulation, inversion, rinsing and protected conveying
Bright beer inlet, optional filtration and controlled pressure and temperature
Low-oxygen filling, end feed, end placement and seaming
Fill level, missing-end, seam and coding checks based on project scope
Warmer, tunnel pasteurizer or bypass according to the approved product strategy
Multipacking, tray or carton packing, palletizing and finished-pack handling
This section defines functional scope only. Equipment count, footprint, rated output, utilities and performance acceptance criteria require project engineering.
Production process
Select a stage to review its operating purpose and handoff. Images illustrate equipment families and are replaced when project-specific media is available.
Accept conditioned beer from the agreed upstream battery limit.
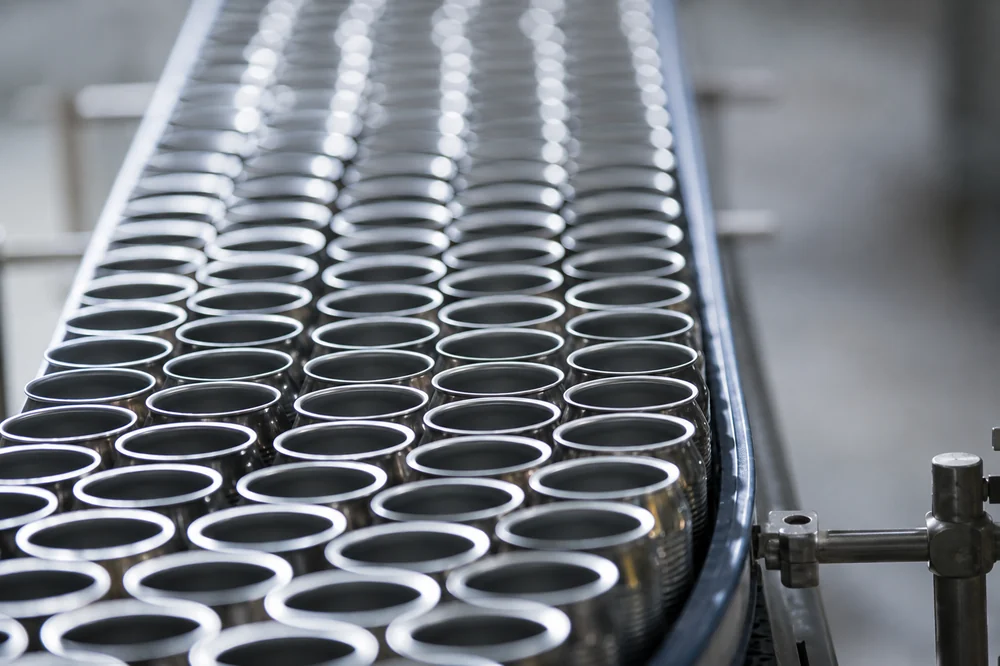
Depalletize, convey, invert and rinse empty cans before they enter the filler.
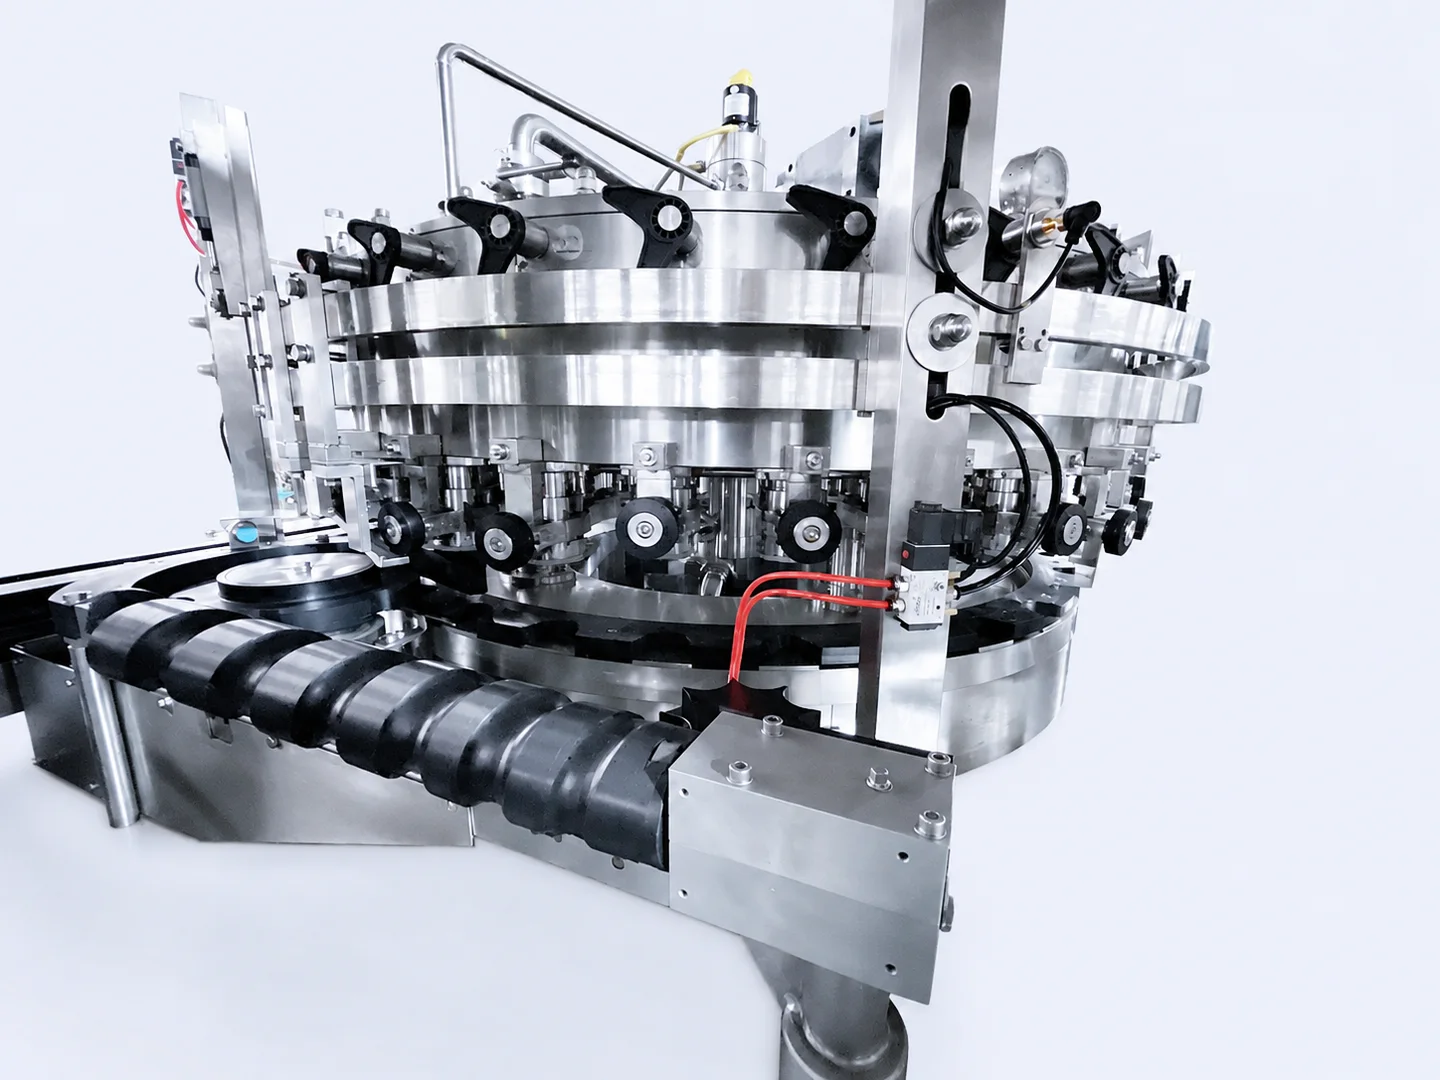
Purge and fill under controlled pressure while managing foam and oxygen pickup.
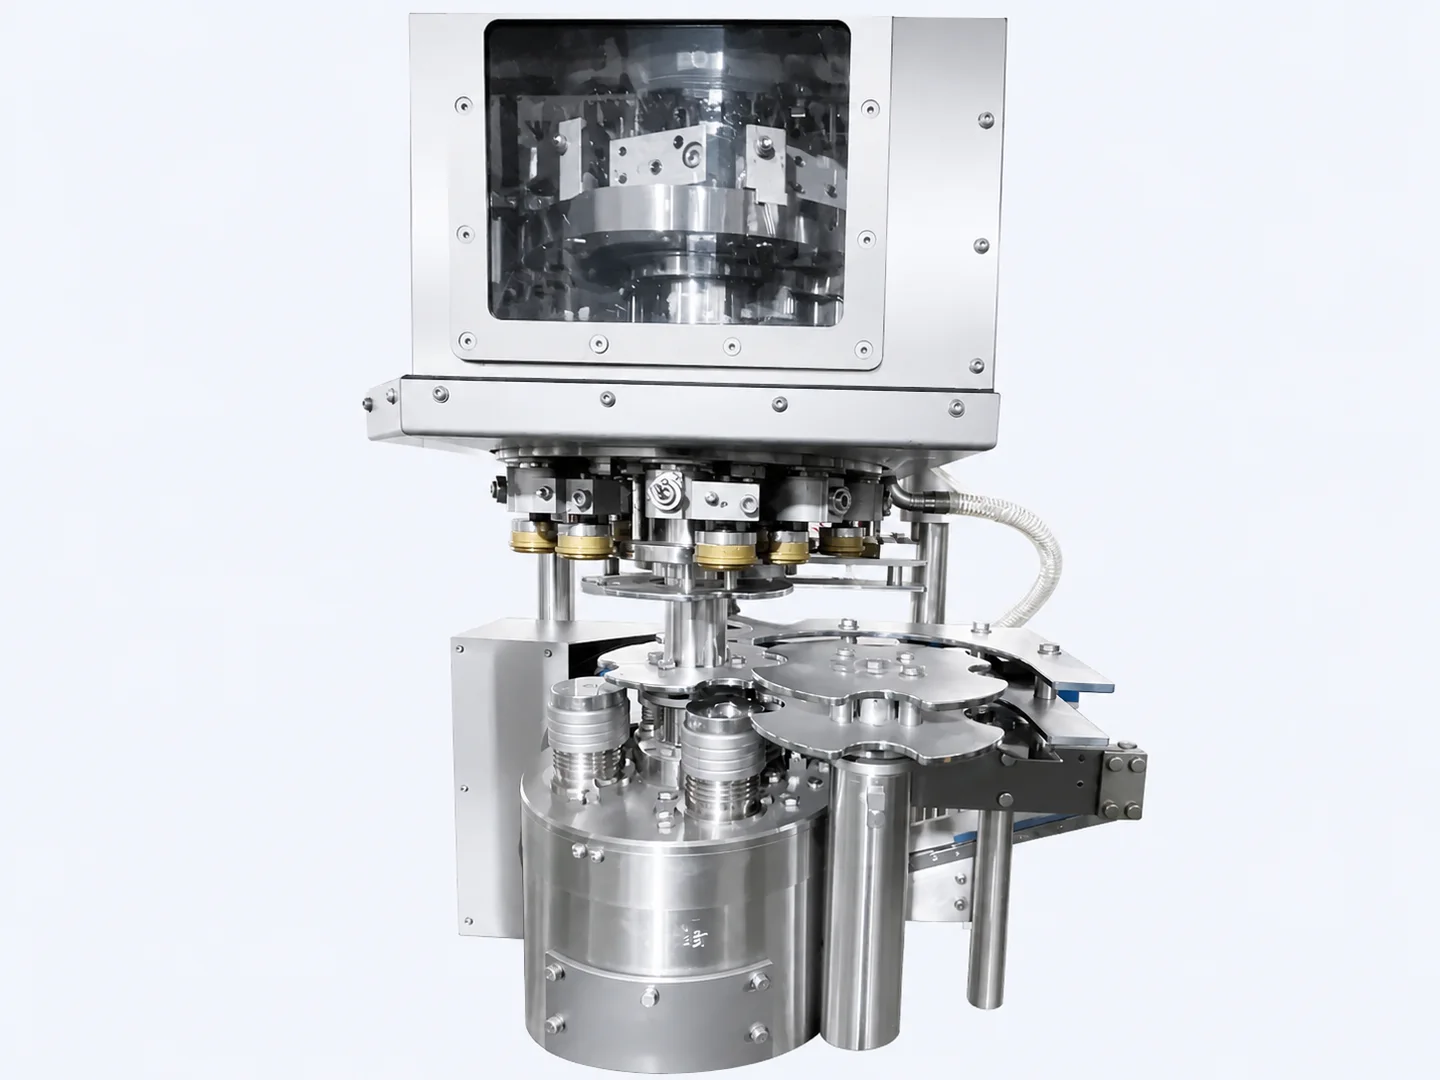
Feed the approved ends, create the double seam and establish routine seam checks.
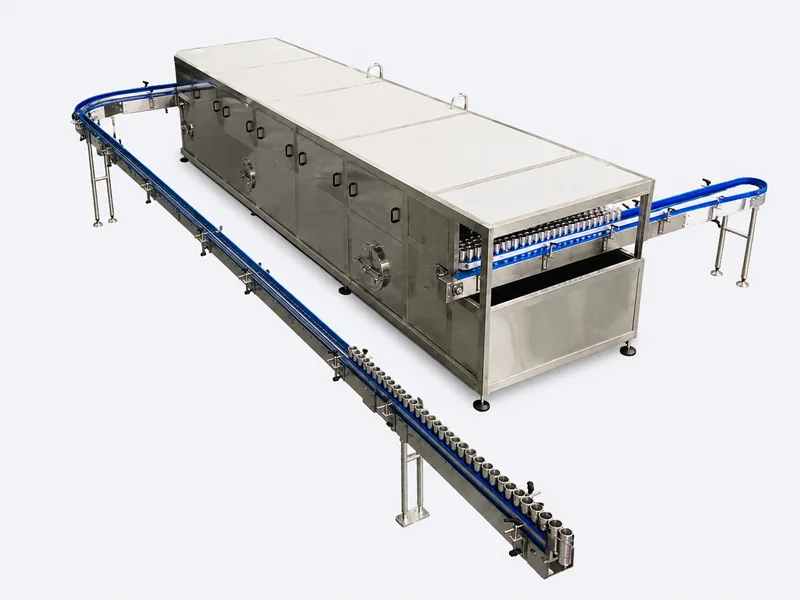
Warm or pasteurize finished cans only when required by the approved process.
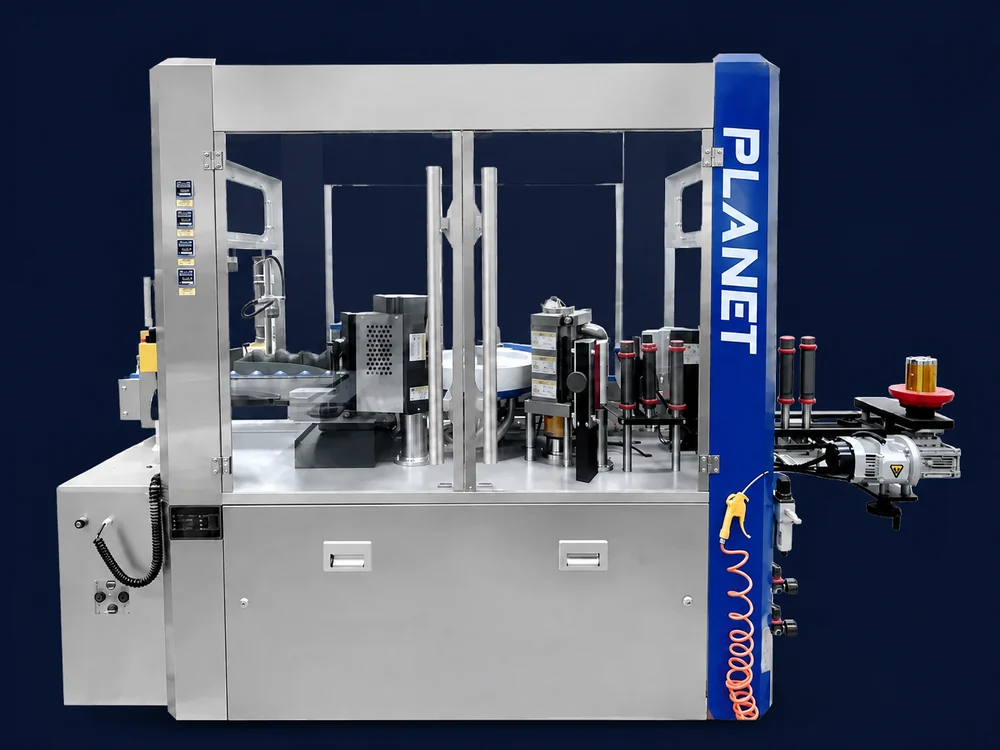
Apply the approved label or decoration and print the required production code.
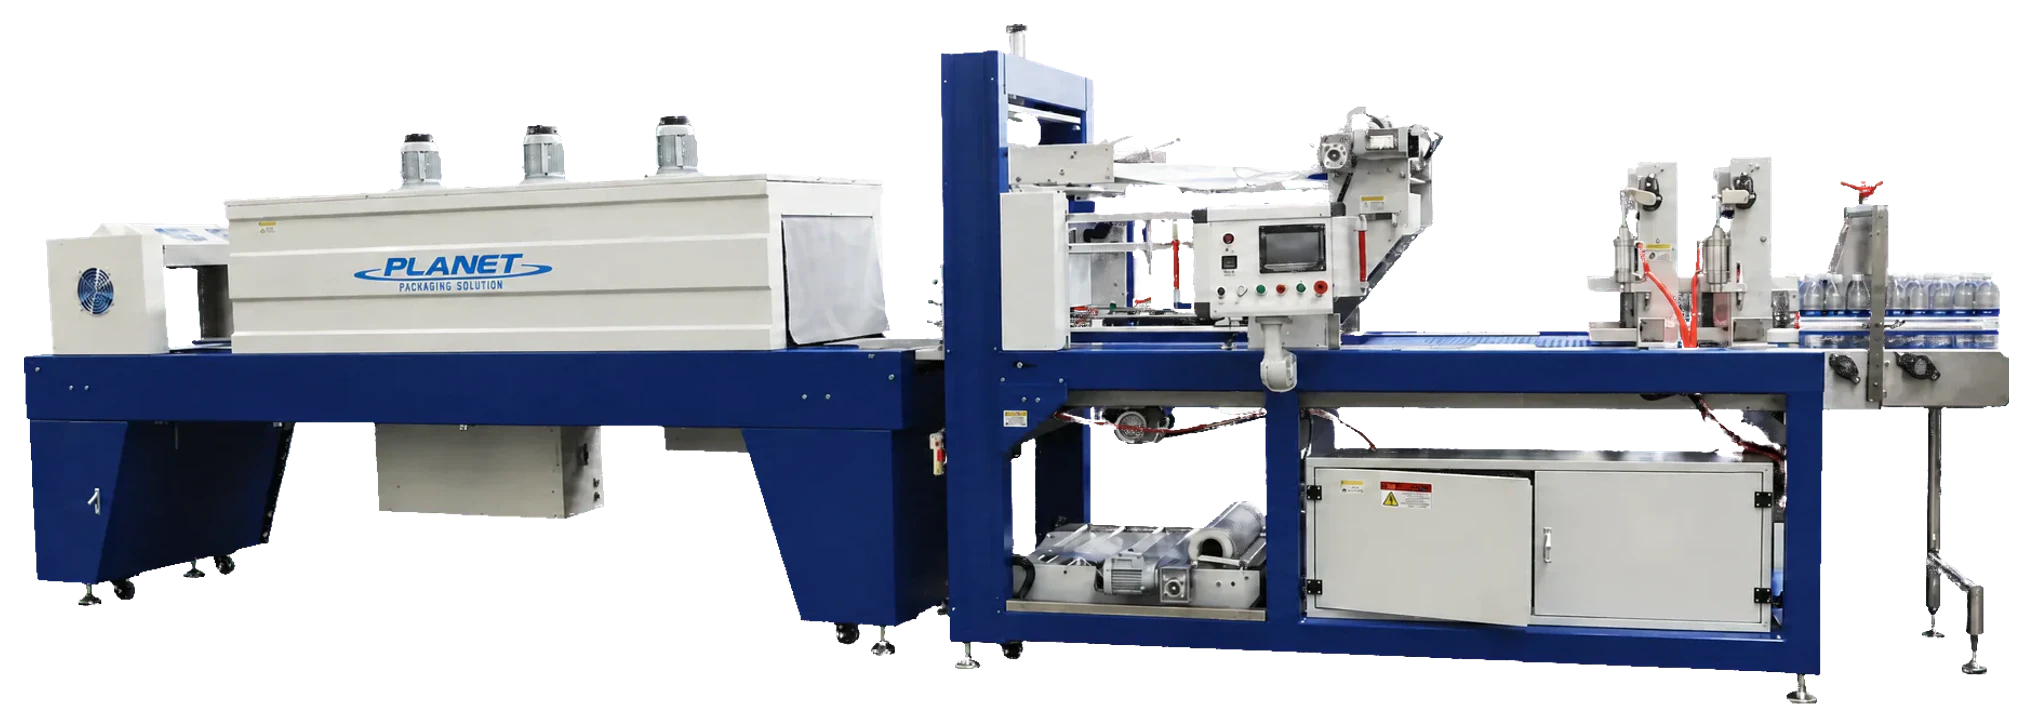
Group finished containers into the confirmed film, tray or carton format.
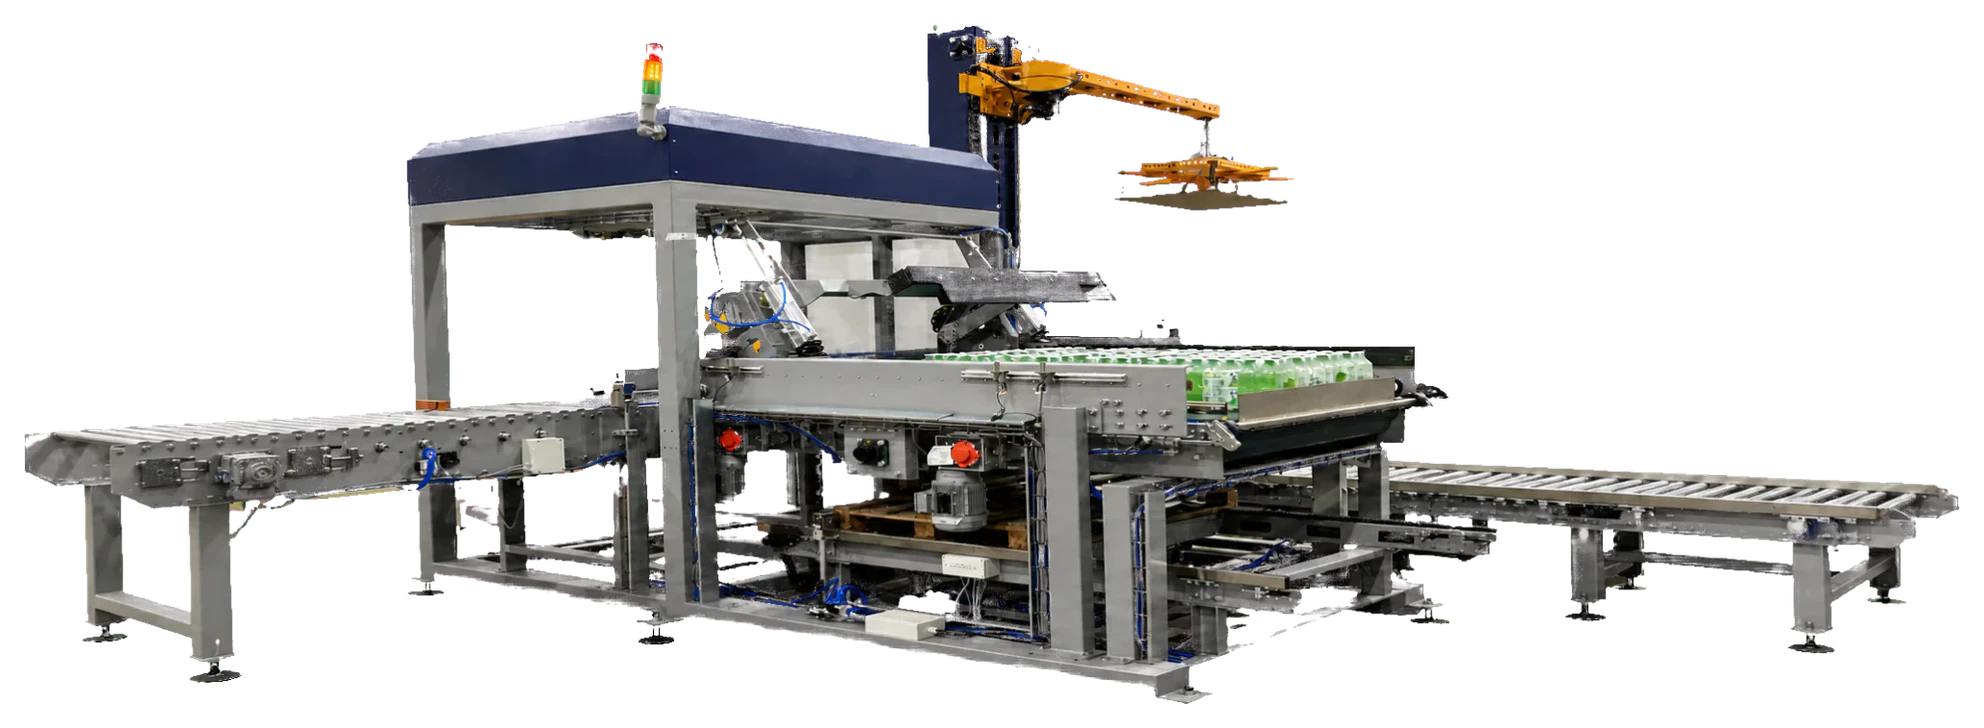
Arrange finished packs for stable warehouse handling and distribution.
Hygiene & quality
Final limits and sampling plans come from the brewer, package suppliers and project acceptance basis—not from a generic catalog.
Define purging and filling control with the brewer.
Protect the flange and reject damaged cans before filling.
Inspect finished-can fill consistency.
Use approved seam measurements and teardown routines.
Confirm cleanable filling paths and repeatable cycles.
Project inputs
Share confirmed facts and mark open questions. The proposal can then separate included equipment, options and assumptions.
FAQ
These answers establish the engineering basis without inventing model ratings or product guarantees.
The double seam is created from the can flange, end curl, compound and seamer tooling. These parts must be approved as a compatible package rather than selected independently.
The solution may combine protected beer transfer, can purging, controlled filling, foam management and rapid end placement. Final targets and measurement points come from the brewer.
No. The thermal route depends on the beer, upstream process, microbiological plan, shelf-life target and distribution conditions.
The quality plan commonly addresses seam dimensions, overlap, tightness, visual defects and teardown frequency. Exact methods and limits must follow the approved can-and-end supplier specification.
Send us the product, package format and target output. We return a line configuration and budgetary quote.
Inquiry received
Our engineering team will respond within 24 hours with a line configuration.
Reference —